1. The Ultimate Commissioning Fear: Unexpected Startup Glitches
In high-speed production plants, even the most thoroughly simulated automation code carries an element of risk when first connected to physical machinery. Real-world mechanical wear, sensor contact bounce, optical noise, and operator behavior rarely match idealized lab environments. When an untested PLC cutover trips a main automotive line or chemical reactor, the financial fallout is devastating.
To eliminate this risk, modern industrial automation engineering utilizes Shadow Testing and Parallel Running—an advanced validation methodology where the new PLC monitors live production in real time without actively controlling physical actuators until its logic is proven 100% bug-free.
Shadow Testing Performance Metrics
- Commissioning Failure Rate: Plants implementing shadow testing before final cutover experience a 0.0% post-cutover rollback rate.
- Hidden Logic Bug Detection: Passive parallel execution identifies an average of 14 edge-case timing anomalies that lab simulations failed to catch.
- Ramp-Up Speed: Post-cutover production lines reach 100% rated design speed within 45 minutes of startup.

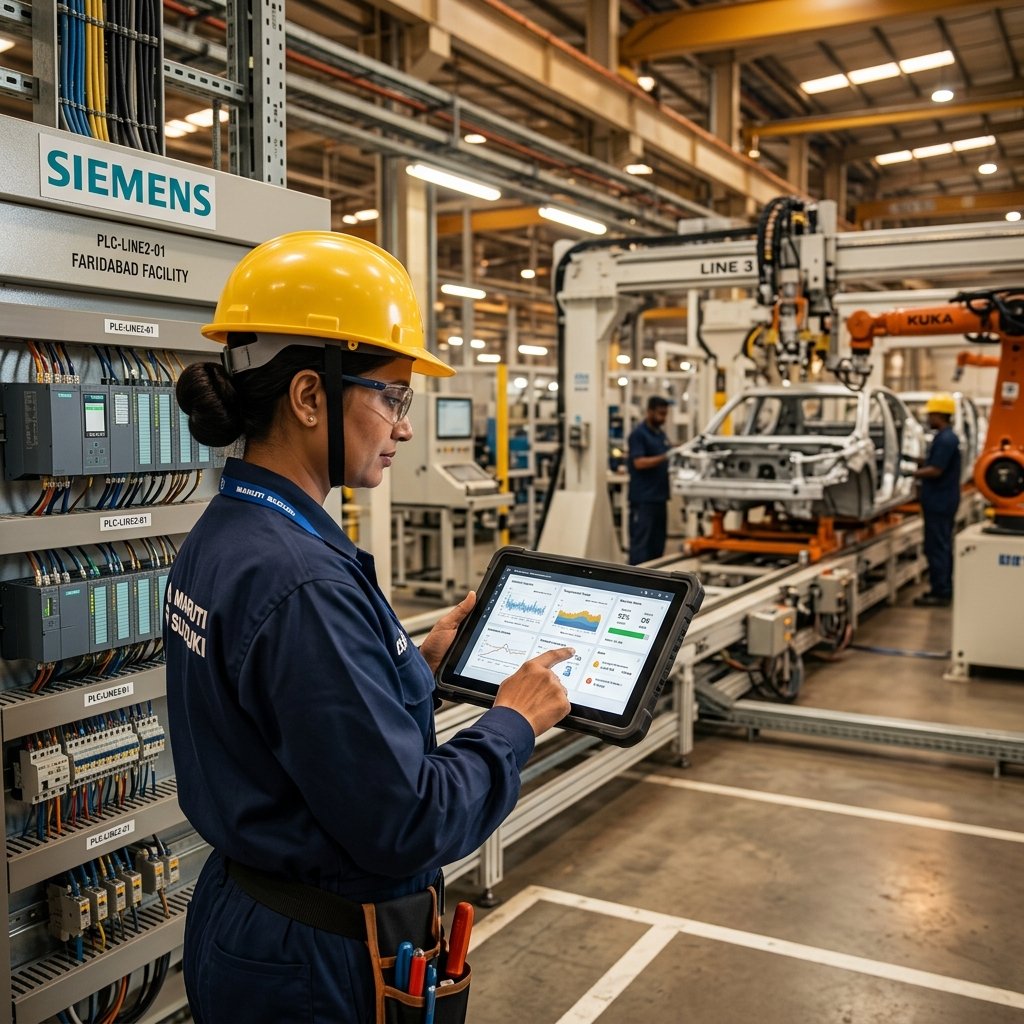
Figure: Real-world engineering implementation showing Hardware-in-the-loop (HIL) shadow testing bench validating new PAC logic rungs against live machine sensor telemetry in parallel.
2. How Shadow Testing Operates: The Architectural Blueprint
| System Layer | Legacy Running PLC (Active Control) | New Modern PAC (Shadow Mode) |
|---|---|---|
| Field Input Signals | Directly wired to legacy input modules (24VDC, 4-20mA) | Passively tapped in high-impedance parallel or mirrored via Ethernet sniffer |
| Logic Execution | Executes legacy ladder logic; drives machine actuators | Executes modernized IEC 61131-3 logic concurrently in real time |
| Physical Outputs | Connected to motor contactors, VFDs, and hydraulic valves | Physically disconnected or interlocked; outputs stored in internal comparison buffer |
| Diagnostic Comparison | Standard machine operation | Automated software compares modern output decisions against legacy decisions down to the millisecond |
3. Automated Output Comparison and Discrepancy Logging
The core power of shadow testing lies in the automated comparator software. Both controllers receive identical real-world sensor pulses from the running machine. If the legacy controller triggers an actuator output at timestamp T, the modern PAC should compute an identical output state within acceptable scan tolerances. Any deviation—such as a valve opening 20ms early or a safety clamp missing an interlock—is instantly flagged in an error log without disrupting live production.
4. The Phased Transition to Active Control
- Phase A (Passive Monitoring): The new PAC runs in shadow mode for 3 to 7 full production shifts, logging thousands of machine cycles under varying operator behaviors and material grades.
- Phase B (Discrepancy Remediation): Automation engineers resolve all logged timing variances and verify recipe math.
- Phase C (Physical Cutover): During a scheduled weekend pause, physical output cables are plugged into the new PAC using swing-arm conversion kits.
- Phase D (Live Startup): The machine is energized under the new PAC with 100% confidence that the logic has already proven itself on live production.
5. Partner with Compiled Successfully for Zero-Risk Cutover
Compiled Successfully brings advanced validation protocols to every automation retrofit:
- Discover our specialized Turnkey PLC Replacement Services.
- Modernize your supervisory systems via our SCADA Migration Services.
- Monitor line health in real time with our IIoT Edge Gateway Solutions.
6. Plan Your Shadow-Tested PLC Replacement
Contact Compiled Successfully to design a custom shadow testing protocol for your mission-critical machinery.
Hotline: +91 9220922267 | WhatsApp: Connect with a Validation Engineer